
 EN


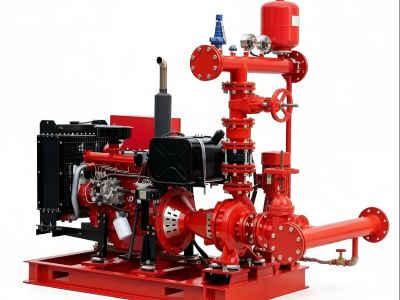
Why Mining Equipment Dealers Should Add Water Pump Products to Their Inventory?
Mining equipment dealers can expand their business opportunities by adding high-quality water pump products to their inventory. Water pumps are essential for mine dewatering, water supply, slurry handling, and mineral processing, making them indispensable in modern mining operations. By offering reliable pumping solutions, dealers can meet a wider range of customer needs while increasing sales and strengthening customer relationships. PREEMINENCE PUMP manufactures durable, high-performance pumping equipment designed to withstand demanding mining environments. In addition to mining applications, the company also provides specialized solutions such as pulp paper pumps, pressure pump systems, and motor pump products for various industrial industries.
What Are the Benefits of Adding Water Pump Products to Your Mining Equipment Inventory?
Water pumps play a critical role in maintaining safe and efficient mining operations. They remove excess groundwater, prevent flooding, and supply water for mineral processing, allowing mining companies to maintain continuous production without costly interruptions. Expanding your inventory with reliable pumping equipment enables customers to purchase both mining machinery and water management solutions from one trusted supplier.
This convenience strengthens customer loyalty while creating additional revenue opportunities for dealers. Modern pressure pump systems also improve operational efficiency by providing stable water pressure for dust suppression, equipment cleaning, and industrial processing. By offering a complete range of solutions, water pump dealers can serve both small mining operations and large-scale industrial projects. Partnering with PREEMINENCE PUMP allows dealers to supply dependable products known for durability, efficiency, and long service life, helping establish long-term relationships with customers across the mining industry.
How to Identify the Best Water Pumps for Mining Applications in Wholesale Markets?
Selecting the right water pumps begins with understanding the specific requirements of each mining application. Different mining operations require different pump designs depending on the type of liquid being handled, flow rate, operating conditions, and pumping distance. For example, mines handling abrasive materials require pumps designed to withstand heavy wear, while clean water applications may require highly efficient motor pump systems that provide reliable performance with lower energy consumption. Durability is another essential factor. Mining equipment operates in harsh environments with mud, sand, rocks, and corrosive materials. Choosing pumps manufactured with wear-resistant materials helps reduce maintenance costs and extend equipment life.
Energy efficiency should also be considered when selecting wholesale products. High-efficiency pumps reduce electricity consumption and lower operating costs for mining water pump companies, making them more attractive to customers.
Dealers should stay informed about industry developments by attending trade exhibitions, reviewing technical publications, and monitoring customer feedback to ensure they continue offering the most effective pumping solutions.
Where to Source High-Quality Water Pump Products for Mining Equipment Dealers?
Working directly with experienced manufacturers is one of the best ways to source reliable mining water pumps. PREEMINENCE PUMP specializes in designing and manufacturing industrial pumping equipment that meets the demanding requirements of mining, construction, and manufacturing industries. Trade shows and industrial exhibitions provide valuable opportunities to evaluate equipment firsthand, compare product performance, and discuss technical specifications with manufacturers. These events also allow dealers to explore complementary equipment such as pulp paper pumps for customers operating across multiple industries.
Developing long-term partnerships with trusted suppliers offers additional benefits, including competitive wholesale pricing, technical support, product training, and priority access to new product releases. Before selecting a supplier, dealers should review product certifications, manufacturing capabilities, warranty policies, and customer feedback to ensure consistent quality and reliable after-sales service.
What Are the Common Usage Issues with Water Pumps in Mining Equipment?
Mining water pumps operate under extremely demanding conditions and may encounter several common performance issues. One of the most frequent problems is clogging caused by rocks, sand, mud, or other abrasive materials entering the pump. Selecting pumps with effective filtration systems and proper impeller designs helps minimize blockages.
Overheating is another common concern, especially during continuous operation. Following recommended operating cycles, performing regular maintenance, and ensuring adequate cooling help prevent excessive temperatures that can damage pump components.
Incorrect pump sizing can also reduce performance. Installing a pump with insufficient capacity may lead to poor water removal, while oversized pumps increase energy consumption unnecessarily. Choosing the appropriate pressure pump or motor pump based on flow rate and head requirements ensures optimal efficiency.
Proper installation and routine inspections are equally important. Regularly checking seals, bearings, impellers, and electrical connections helps identify potential problems before they result in costly downtime or equipment failure.
How to Market Water Pump Products Effectively to Attract Wholesale Buyers?
Successful marketing begins with understanding the needs of mining companies, contractors, and industrial customers. Creating informative product pages that clearly explain specifications, applications, and performance advantages helps buyers make confident purchasing decisions. A professional website featuring PREEMINENCE PUMP products, detailed technical information, and application examples can significantly improve customer engagement.
Demonstrating how products such as motor pump systems and pressure pump solutions improve operational efficiency adds value for potential buyers. Social media platforms and video demonstrations are also effective marketing tools. Showing high pressure centrifugal water pump operating in real mining environments helps customers understand product reliability and performance under demanding conditions.
Participating in mining exhibitions and industrial trade shows allows dealers to meet prospective customers, demonstrate equipment, and build valuable business relationships. Offering introductory promotions, volume discounts, and responsive after-sales support further encourages wholesale buyers to choose your products. Finally, maintaining strong communication with existing customers encourages repeat business and referrals. By combining high-quality products, expert technical support, and excellent customer service dealers can establish themselves as trusted suppliers of mining water pumps and related industrial pumping solutions, including pulp paper pumps, pressure pump systems, and motor pump products.
Table of Contents
- Why Mining Equipment Dealers Should Add Water Pump Products to Their Inventory?
- What Are the Benefits of Adding Water Pump Products to Your Mining Equipment Inventory?
- How to Identify the Best Water Pumps for Mining Applications in Wholesale Markets?
- Where to Source High-Quality Water Pump Products for Mining Equipment Dealers?
- What Are the Common Usage Issues with Water Pumps in Mining Equipment?
- How to Market Water Pump Products Effectively to Attract Wholesale Buyers?